A retort pouch shape that looks ideal on shelf may complicate filling, processing, or packing. I compare the full workflow before choosing the format.
I choose a three-side-seal retort pouch when flat handling, controlled headspace, retort loading, and compact case packing lead the brief. I choose a stand-up format when upright shelf use justifies the gusset. The processor must validate the final package and scheduled process.
The correct answer depends on more than appearance. I review the product, line, retort system, distribution case, and consumer use as one connected specification.
What Is the Practical Difference Between the Two Retort Pouch Formats?
Buyers often compare only the front panel. That view hides the bottom construction that changes standing behavior, dimensions, filling, and handling.
A three-side-seal retort pouch is a flat format sealed on three sides and normally supplied with one side open for filling. A stand-up retort pouch adds a bottom gusset so the filled pack can form a base. Both still require a process-specific laminate, seals, and validation.
I start with geometry, not a marketing label
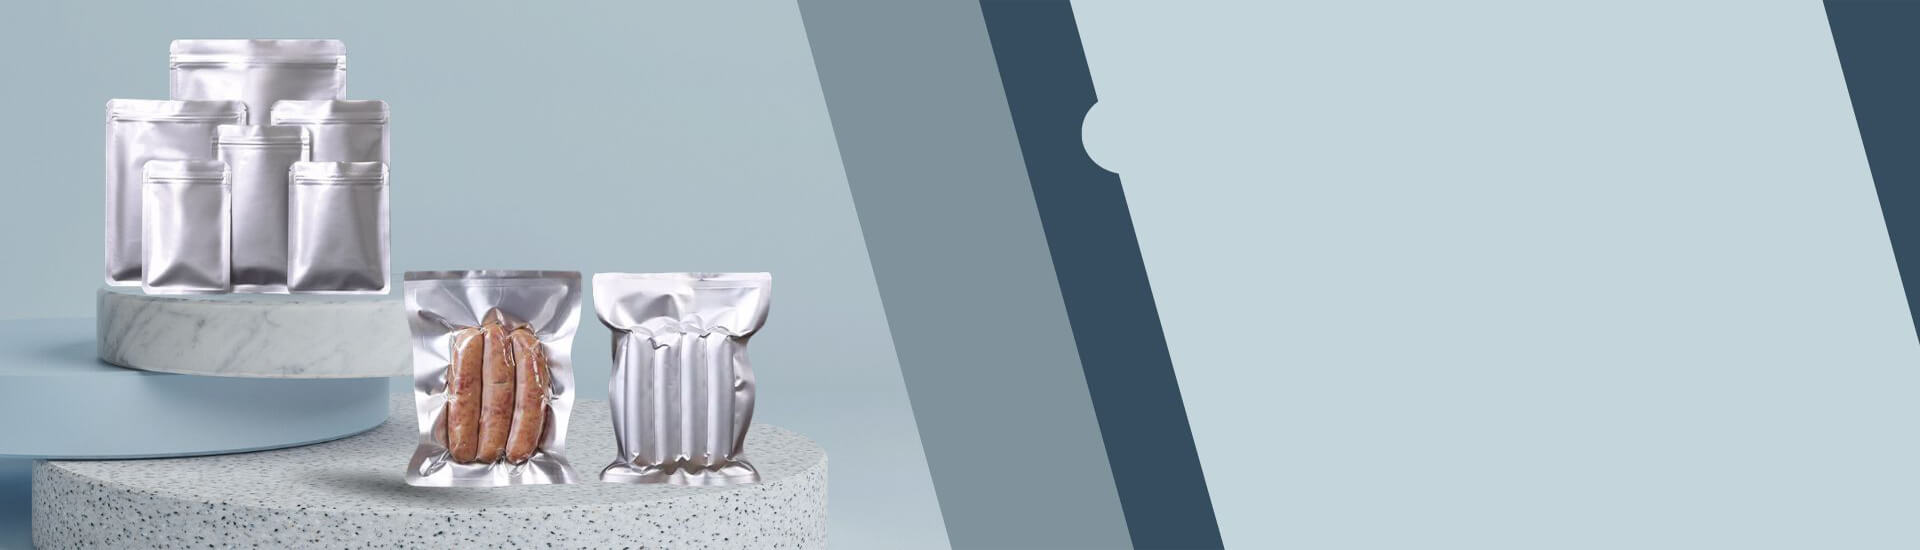
The three-side-seal format has two main panels and no expanding bottom base. It usually lies flat before and after filling, although the product shape affects its final profile. The stand-up format includes extra folded material at the bottom. That gusset opens as the pouch fills and can support an upright presentation when the pouch, fill volume, and distribution conditions work together.
The word “stand-up” does not guarantee that every filled pouch will stand reliably. A narrow pouch, an uneven product, too little fill, trapped product in the gusset, or an unsuitable base proportion can change stability. I therefore ask buyers to test the actual product rather than approve an empty display sample.
| Decision point | Three-side-seal format | Stand-up format |
|---|---|---|
| Empty construction | Flat two-panel body | Body with a bottom gusset |
| Shelf posture | Usually displayed flat or supported | Designed for possible upright display |
| Dimensional focus | Width, height, seal zones, fill opening | Width, height, gusset, seal zones, fill opening |
| Main operational question | Does the flat pack suit loading and retort arrangement? | Does the gusset open, fill, process, and stand as intended? |
| Approval method | Filled and processed sample | Filled, processed, cooled, and standing sample |
Our retort bag product page confirms that XINYUAN works in this product category. I still treat every new application as a separate packaging project. I do not infer food-contact suitability, thermal-process suitability, or shelf life from the pouch shape alone.
How Do Filling, Sealing, and Retort Handling Affect the Choice?
A pouch can pass a visual review yet slow the line or sit poorly in a retort rack. The packing sequence must guide the format decision.
I favor the format that the filler can open, dose, clean, close, and place consistently. Buyers should compare mouth access, product flow, headspace control, seal contamination risk, vacuum needs, pouch restraint, retort orientation, cooling, and unloading with representative product.
I map every handling step
I ask the buyer to show how an empty pouch reaches the filling point and how the equipment grips it. A flat pouch can be straightforward to present, but the exact opening and fixture still matter. A stand-up pouch introduces a gusset that must unfold predictably. Product must enter the body without lodging in a seal area or preventing the base from opening.
After dosing, the line may remove air, control headspace, clean the sealing zone, and make the final closure. Those requirements come from the product and the validated process, not from a generic pouch recommendation. Liquids, sauces, solid pieces, and mixed products behave differently during filling and heating. I ask for representative contents because water alone may not reproduce the actual flow or distribution.
The processor and its qualified process authority must determine the scheduled process and critical factors. For products subject to United States low-acid canned food requirements, 21 CFR Part 113 addresses scheduled processes and control of critical factors. Other destinations and products can have different requirements. I use this official source to explain why package geometry cannot be changed casually; I do not present it as legal advice or claim that a specific XINYUAN pouch is approved.
The buyer should trial the chosen format in the actual basket, rack, divider, or restraint arrangement. The test should cover loading density, pouch position, movement, contact points, heating, cooling, unloading, and post-process inspection. A gusseted pouch may offer display advantages, but those advantages do not replace process validation.
How Do Shelf Display and Secondary Packing Change the Decision?
Retail teams may prefer an upright pouch while operations teams prefer a flat one. An early pack-out test helps both teams make one commercial decision.
A stand-up retort pouch can provide an upright facing and broader shelf presence. A three-side-seal pouch can suit flat display, cartons, trays, or compact case arrangements. Buyers should compare the processed pack, not an unfilled mockup, because heating and cooling can change its shape.
I evaluate the package after processing
The finished package is the product the retailer and consumer receive. I therefore check how the pouch looks after filling, sealing, retorting, cooling, drying, and case packing. The stand-up pouch must form a usable base and remain acceptably stable with the actual contents. The flat pouch must fit its intended tray, carton, peg, shelf, or outer pack without creating unwanted folds or pressure points.
Artwork also follows the finished geometry. A bottom gusset consumes and bends print area. Important copy, codes, or instructions should not disappear into a fold or sit across a zone that changes shape. On a flat pouch, product thickness can still distort the front panel, so the artwork proof should be checked on a filled sample. XINYUAN provides free artwork and typesetting service, which can help align the design with the approved dieline. The buyer remains responsible for required label content in each destination market.
I compare logistics with retail value
I ask buyers to build both candidate formats into their real shipping case. They should record the number of units per case, orientation, dividers if used, case dimensions, pallet pattern, and damage observations from their own distribution trial. A stand-up pouch can earn its added structural complexity when upright presentation materially supports the brand or consumer experience. A flat format may be more practical when the pouch is sold in a carton, displayed horizontally, or used as an ingredient pack.
The decision should use total system value rather than pouch price alone. Filling speed, line changes, retort capacity, secondary packaging, shelf presentation, and complaint risk can outweigh a small unit-price difference.
What Should Buyers Validate Before Approving Bulk Production?
Changing only the pouch outline can change several process conditions. A controlled approval plan keeps shape, material, seals, artwork, and thermal processing connected.
Buyers should approve a dimensioned drawing, construction specification, filled sample, sealing trial, retort trial, distribution pack-out, finished appearance, opening method, and inspection plan. Any change to size, gusset, fill weight, product, seal, laminate, orientation, or process should trigger formal review.
I ask for a controlled specification package
The drawing should show overall width and height, bottom-gusset geometry when applicable, corner shape, seal locations, seal width targets defined by the project, open filling side, tear notch, coding area, and artwork limits. The specification should identify the agreed laminate and the intended product and process without assuming that one construction suits every recipe or retort cycle.
The buyer should also record the filling equipment, sealing equipment, product condition at filling, target fill control, headspace or vacuum requirement set by the process authority, retort type, pouch orientation, restraints, cooling method, and inspection criteria. This creates a traceable basis for the custom sample and bulk order.
| Approval stage | Evidence I request from the buyer or trial |
|---|---|
| Drawing review | Signed dimensions, gusset, seals, opening, and artwork version |
| Line trial | Consistent opening, filling, cleaning, and sealing behavior |
| Process review | Written acceptance by the responsible processor and process authority |
| Retort trial | Approved loading pattern and post-process package inspection |
| Distribution trial | Accepted case pack, handling result, and shelf presentation |
| Bulk release | Agreed inspection method and change-control contacts |
I use samples to reduce avoidable risk
I can provide free in-stock samples for an initial review of workmanship and general format. A separately produced custom sample may require a sample fee. If a later bulk order follows, I can return that fee or deduct it from the bulk-order price, subject to the confirmed quotation. A stock pouch is not proof that a custom pouch will suit the buyer's food, scheduled process, filling line, or market.
As a packaging bag manufacturer, XINYUAN has dozens of production machines and an integrated production system covering raw-material production through finished products. Our equipment, experienced employees, and production organization support large orders and long-term supply. I present that as our operating capability and focus, not as an unconditional performance guarantee. The safest bulk decision still begins with buyer-approved specifications and process-specific evidence.
Conclusion
I choose a retort pouch format by testing the complete system: product, filling, sealing, processing, case packing, shelf presentation, and controlled bulk specifications.